Pioneering standard-grade isolated soy proteins, high-purity ethanol, and functional cereal proteins.
In the contemporary landscape of global food processing and alternative protein development, Vital Wheat Gluten (VWG) stands as an irreplaceable structuring agent. Sourced from high-quality wheat flour, VWG contains a natural, highly functional protein matrix composed mainly of gliadin and glutenin. When hydrated, these proteins align to form a viscoelastic network capable of retaining gas, trapping moisture, and providing a dense, fibrous texture that closely mimics animal muscle fibers.
The global demand for Vital Wheat Gluten is currently experiencing a compound annual growth rate (CAGR) of over 5.2%, driven primarily by the rapid expansion of the plant-based meat sector, clean-label clean-ingredient movements, and the functional fortification of standard bakery items. For large-scale food manufacturers, securing a consistent, high-purity supply of wheat gluten is vital to maintain production efficiency and consistency.
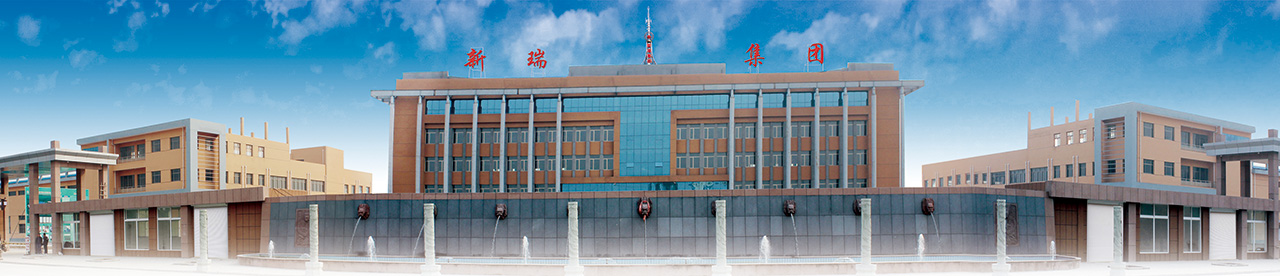
Leveraging state-of-the-art agricultural supply chains to produce premium wheat proteins, starches, and value-added derivatives.
Established in 2007 with a registered capital of 100 million Yuan. We process over 500,000 tons of high-grade wheat flour annually. Our industrial pipeline isolates vital wheat gluten, wheat starch A, and wheat starch B utilizing zero-waste principles.
Founded in 2014 with 120 million Yuan registered capital. Processing 180,000 tons of domestic Non-GMO soybean annually, extracting non-GMO soy oil, low-temperature soy meal, isolated soy protein (ISP), and dietary fiber.
Established in 2011 to handle the group's global exports. Directing over 70% of factory production to global partners in North America, Europe, Southeast Asia, and the Middle East, offering a streamlined supply chain.
Tons Wheat Processed Annually
Tons Non-GMO Soy Processed
Annual Value (Yuan)
Export Volume Ratio
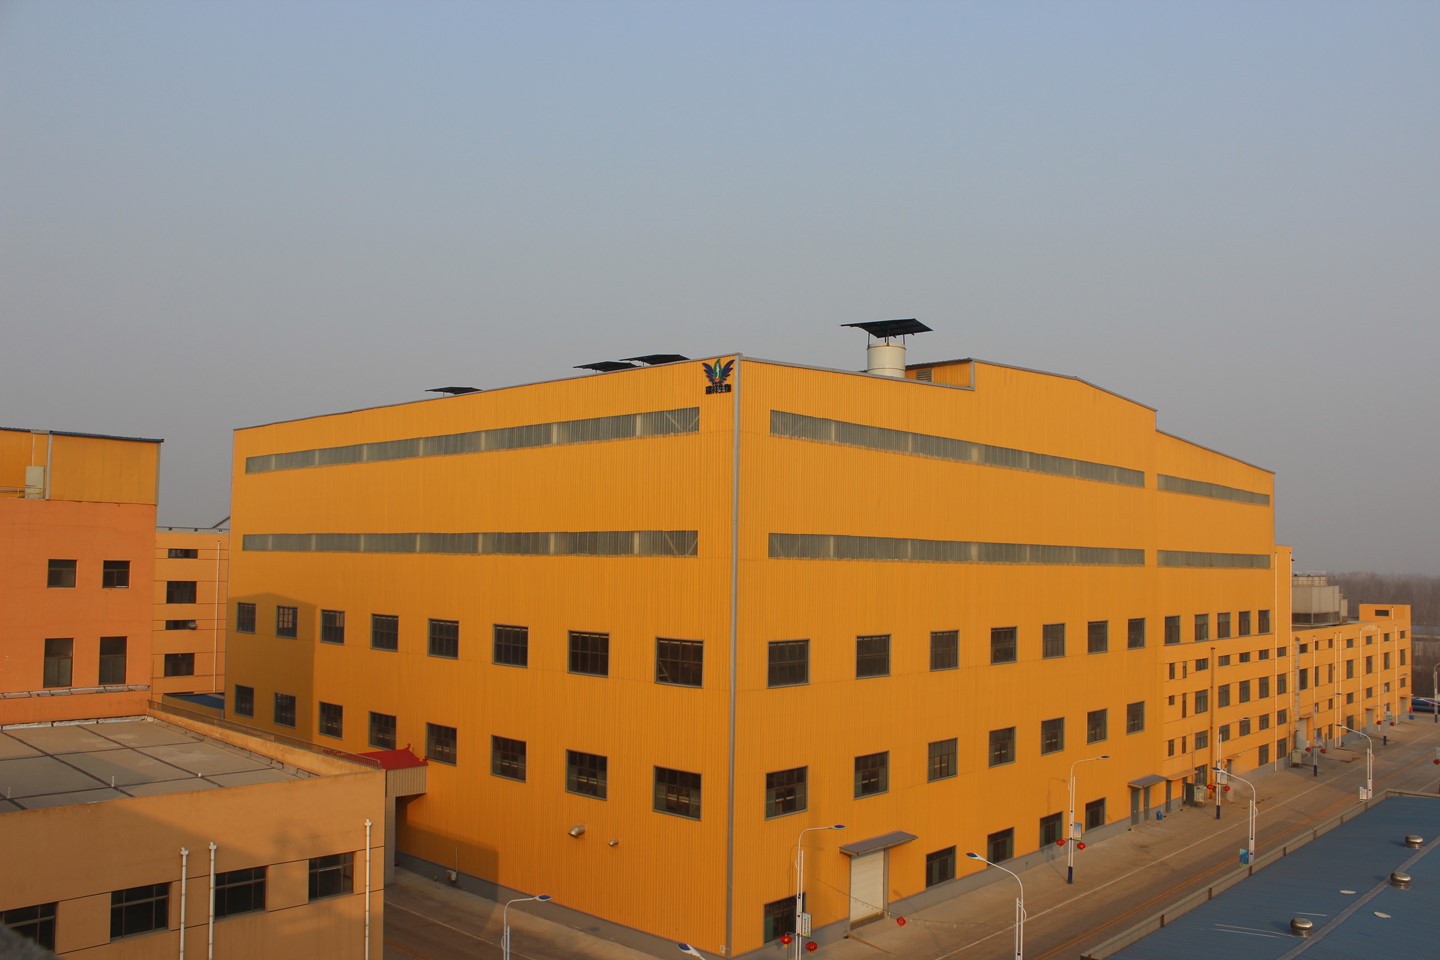
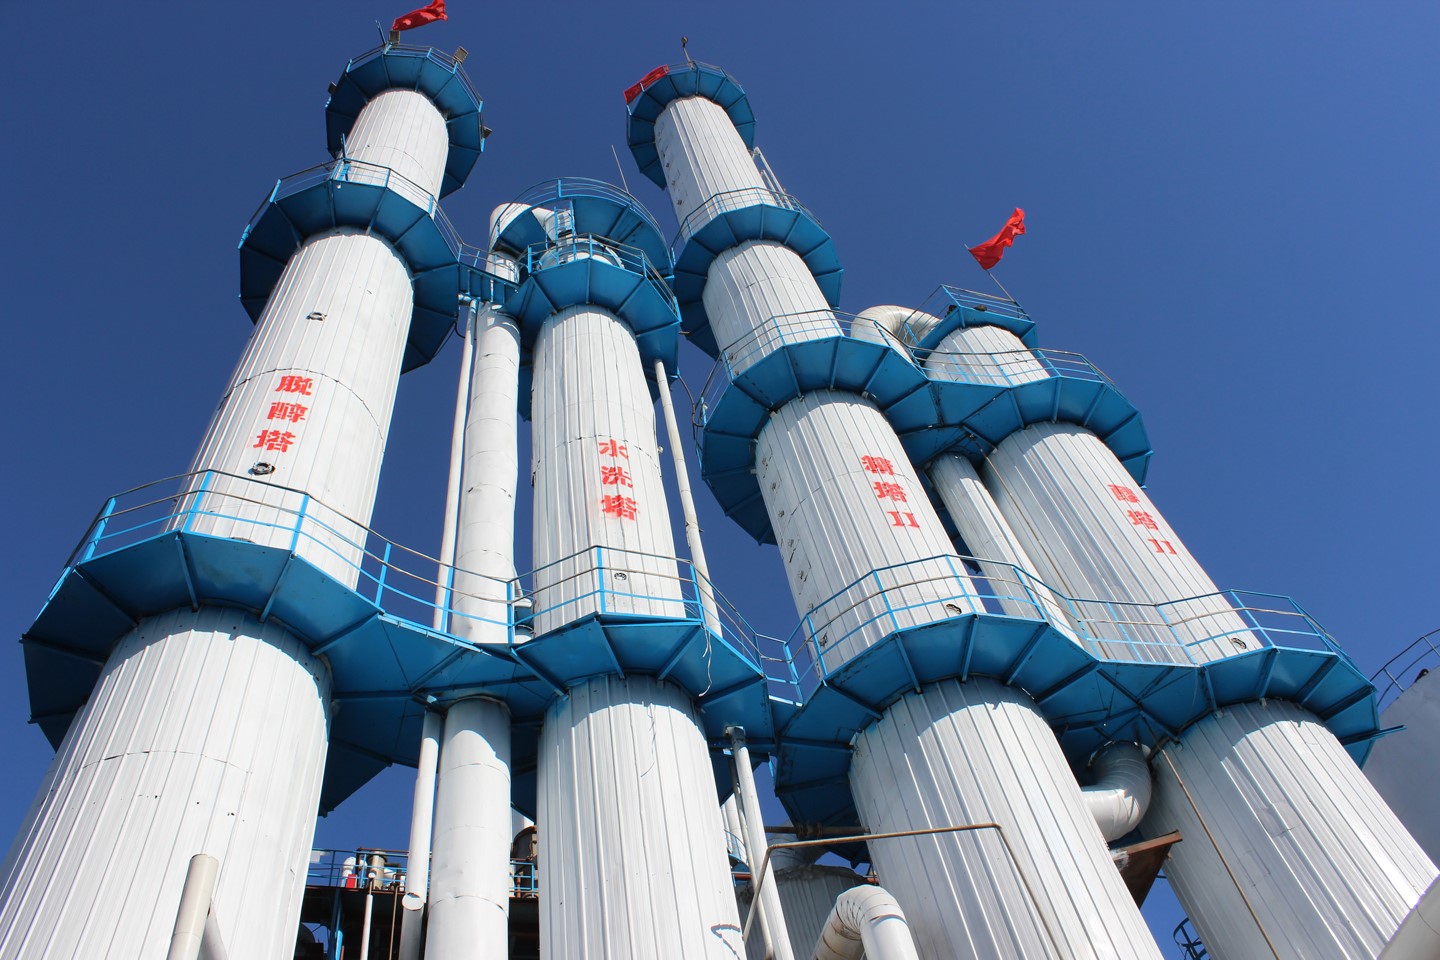
Securing high protein content and consistent viscoelastic properties in Vital Wheat Gluten requires precise wet-milling. We utilize state-of-the-art, imported tri-canter separation technology. Unlike traditional wash systems, this closed-loop method operates in a sanitized environment to isolate the constituents of the wheat kernel based on density differentials.
Premium wheat flour is combined with purified water, letting the gluten proteins fully hydrate and form a cohesive matrix, separating them from free starch granules.
The hydrated slurry is passed into a high-speed three-phase centrifuge (Tri-canter) to continuously separate Vital Wheat Gluten, high-density Starch A, and lower-density Starch B/pentosans.
To prevent heat damage to the delicate protein structure, the wet gluten is dried using a rapid flash ring dryer. This protects its vital elasticity and water absorption capacity.
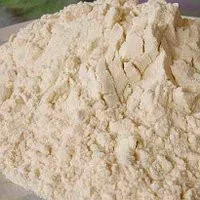
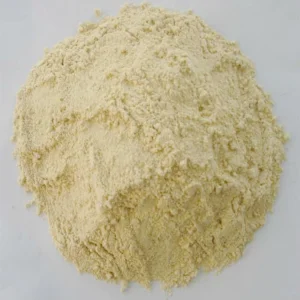
The dry product is either milled into a fine powder (VWG-P) or compressed into pellets (VWG-PS) to optimize shipping bulk density and prevent dust during transport.
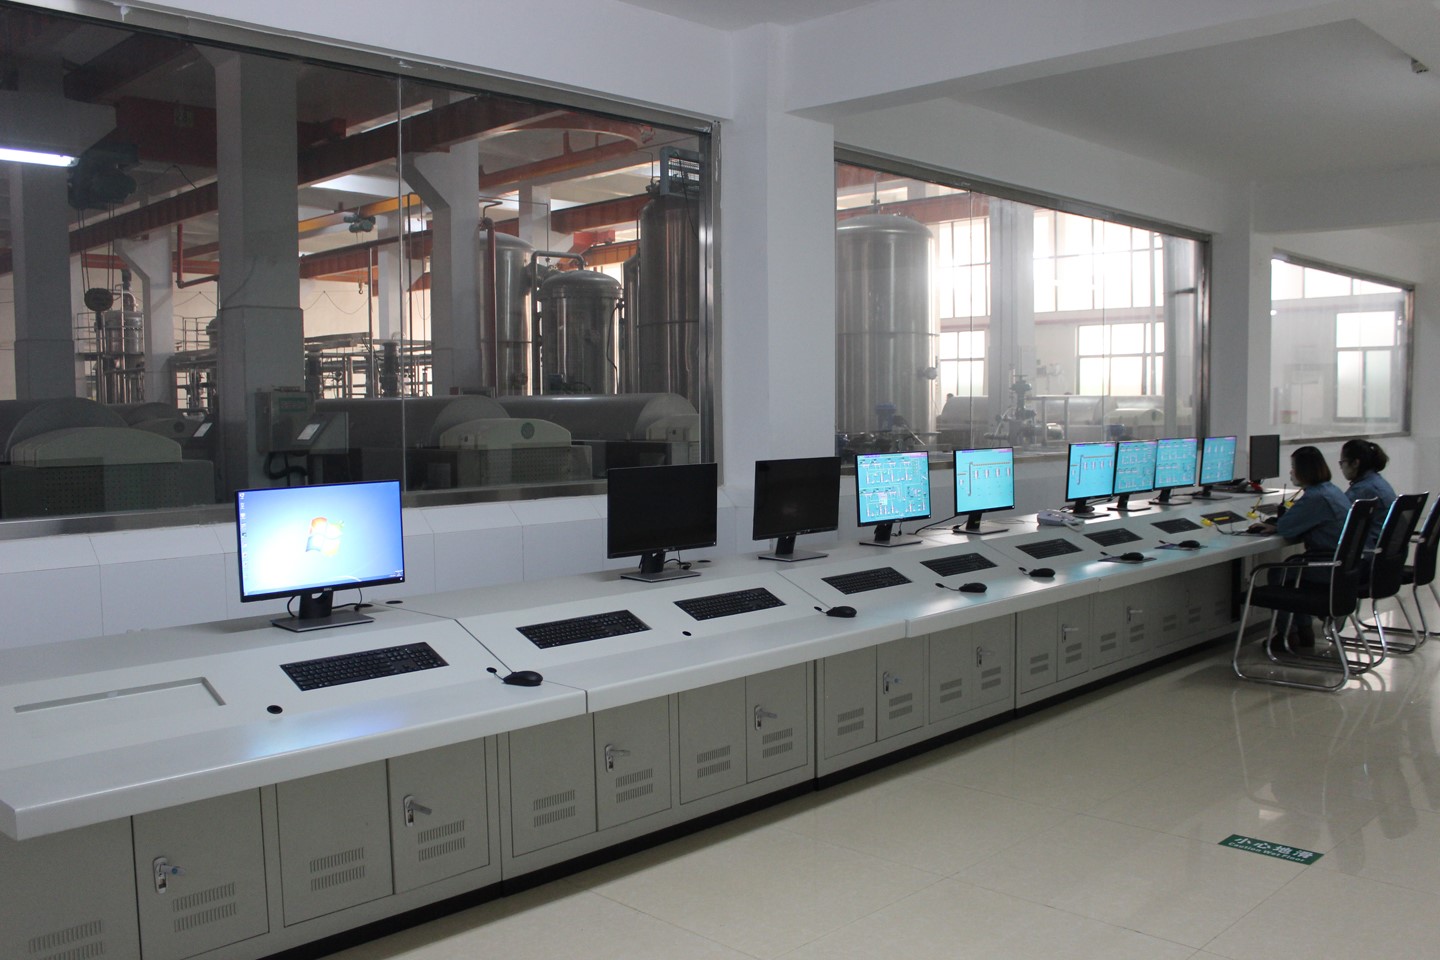
Scientific Note: The functional quality of wheat gluten is determined by its water absorption index (typically >150%) and viscoelastic recovery. By avoiding high thermal stress in the flash dryer, we keep the native molecular structures intact, ensuring excellent performance for our customers.
Tailored technical properties designed to meet the demands of global food, aquaculture, and animal feed industries.
In regions with low-protein wheat harvests, adding vital wheat gluten is a cost-effective way to improve flour strength. It strengthens the dough structure, increases bread volume, improves crumb texture, and helps the final product stay soft and fresh longer.
For vegetarian products and meat substitutes, wheat gluten is essential. Its fibrous protein network creates a realistic, chewy texture. It works well with soy proteins to hold water and fat, improving the overall bite and taste.
Because of its high protein content (>75% on dry basis) and excellent digestibility, our vital wheat gluten is widely used in premium fish feeds and pet foods. It acts as a natural binder, helping feed pellets stay together in water without using chemical additives.
Take an inside look at our advanced production facilities, automated processing lines, and quality verification systems.
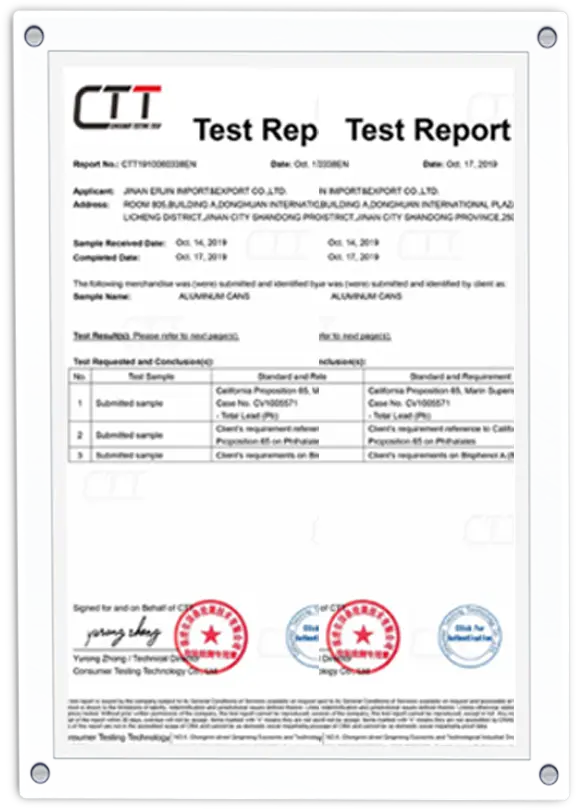
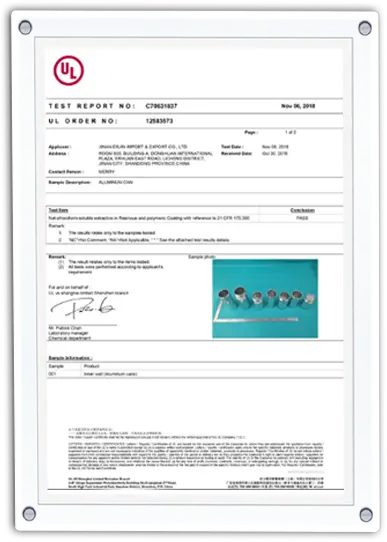
Committed to international quality standards through third-party audits and certifications.
Addressing technical questions about our wheat proteins, isolated soy proteins, and industrial capabilities.
We are an integrated group company named Xinrui Group that handles both manufacturing and exports. Production of soy protein isolate is managed by our subsidiary, Shandong Kawah Oils Co., Ltd, which has an annual capacity of 50,000 tons. Our vital wheat gluten is manufactured by Guanxian Xinrui Industrial Co., Ltd. (formerly Guanxian Ruixiang Biotechnology Development Co., Ltd) with an annual capacity of 30,000 tons. Global export operations are managed by Guanxian Ruichang Trading Co., Ltd.
Our production facilities maintain strict quality management systems and are certified under HACCP, ISO9001, ISO22000, BRC, HALAL, KOSHER, and IP-NON GMO. We also provide SGS inspection reports and export documentation tailored to your country's customs regulations.
Our standard Vital Wheat Gluten powder (VWG-P) has a protein content of ≥ 75% (on a dry basis), with moisture levels kept below 9.0%. This keeps the protein active and ensures stable viscoelastic properties when hydrated.
Our closed-loop Tri-Canter system keeps processing temperatures low. This prevents the gluten from denaturing early, ensuring it maintains a high water absorption capacity (at least 150-180% of its dry weight) and strong gas retention properties during baking.
Yes. We offer Vital Wheat Gluten in 25kg multi-paper bags, 1-ton bulk bags, and compressed pellets (VWG-PS) for easier bulk handling and reduced dust. Our logistics team handles direct ocean shipments to ensure timely delivery and low freight costs.
Providing consistent quality and functional performance for food processors worldwide.
 Xinrui Group