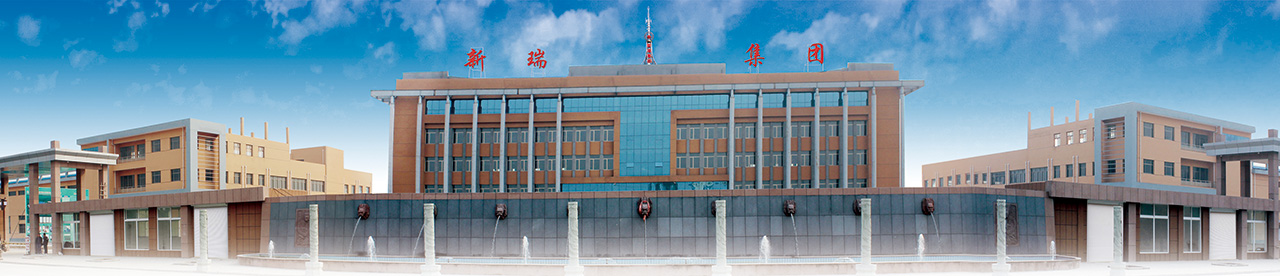
XINRUI GROUP was established in May 2003, covering a total area of more than 1,000 mu, and has evolved into an exemplary diversified industrial group enterprise with an annual output value exceeding 2.8 billion yuan. By integrating agriculture, advanced research and development, large-scale deep processing, and direct global import & export, our industrial matrix ensures uncompromised quality control across every supply chain tier.
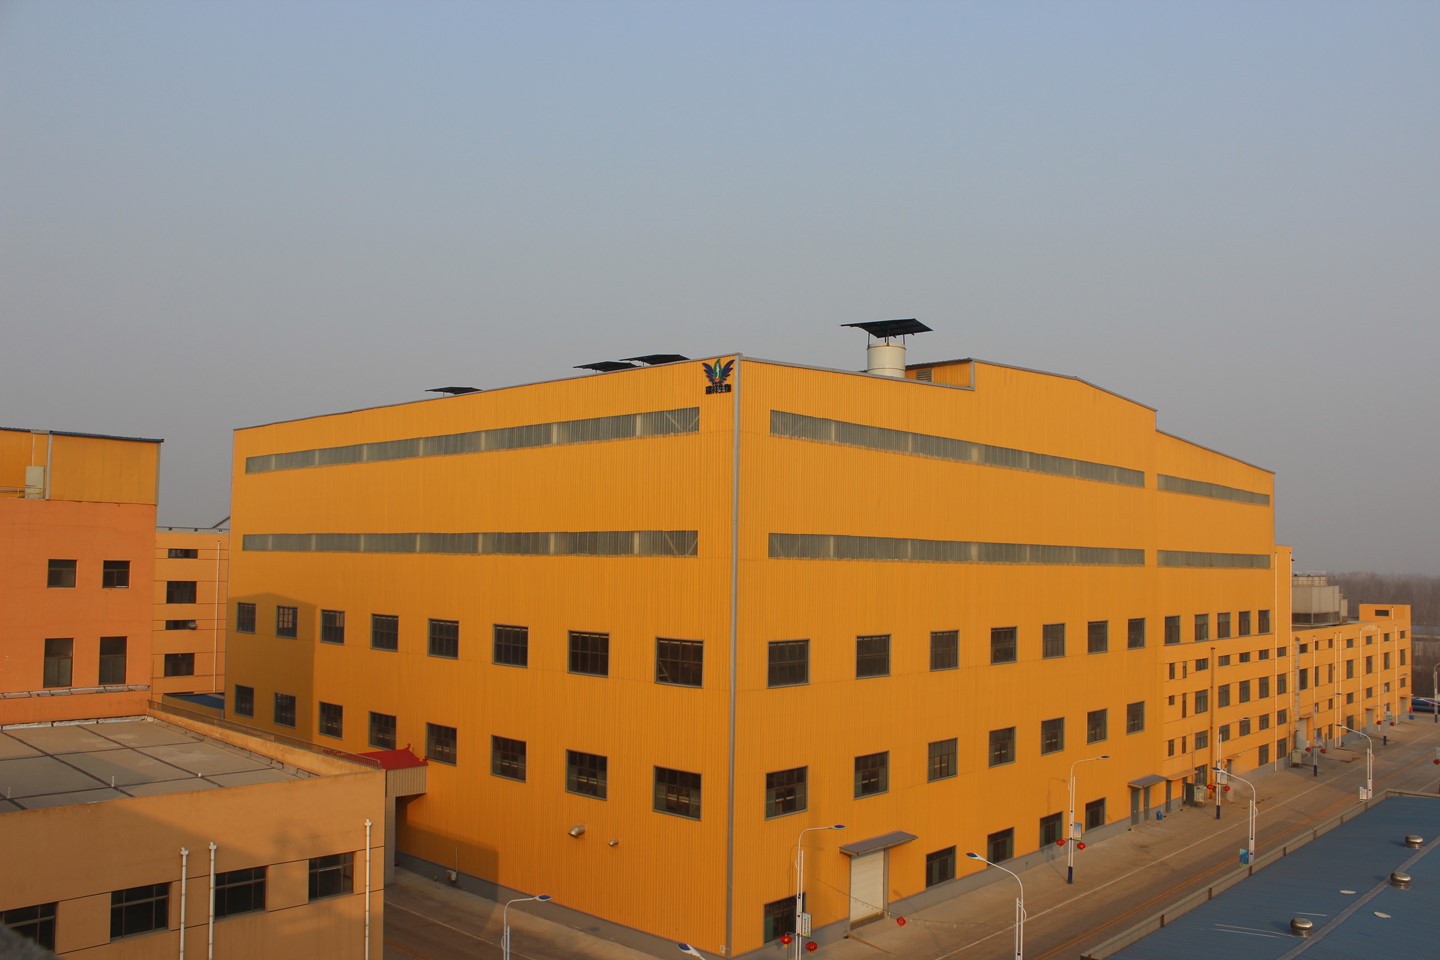
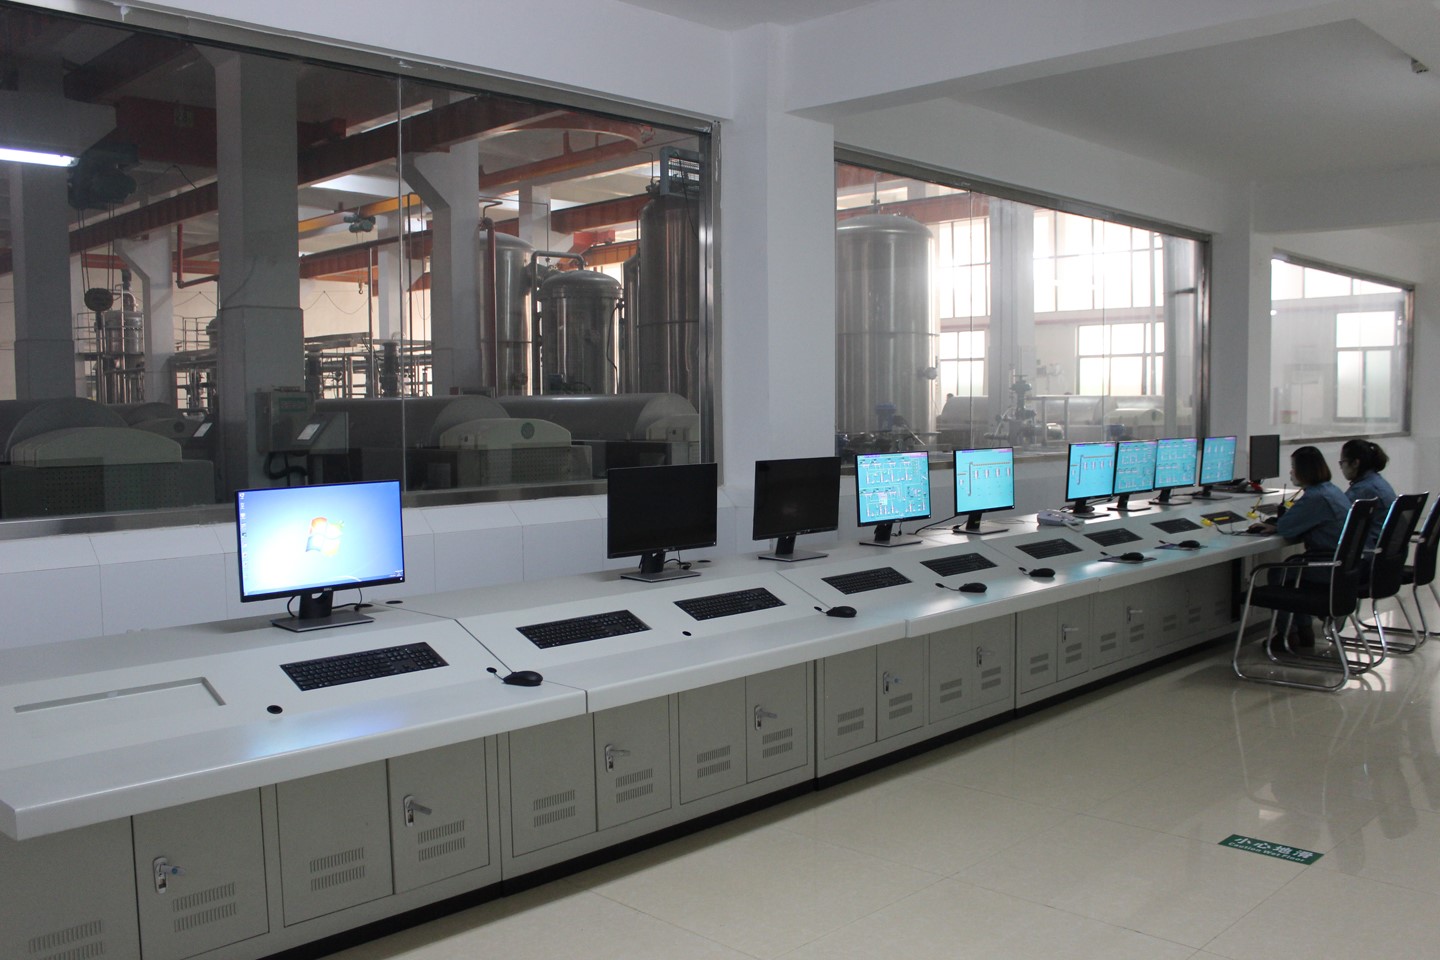
Formerly known as Guanxian Ruixiang Biotechnology Development Co., Ltd, founded in 2007 with a registered capital of 100 million Yuan. We process 500,000 tons of high-grade wheat annually, utilizing state-of-the-art tri-decanter separation technology imported from industry leaders. Our production lines operate in a strictly clean, closed-loop environment, producing premium vital wheat gluten, wheat starch A, and wheat starch B. Byproducts such as starch B and pentosan are systematically channeled into circular economy streams for alcohol and animal feed production, reinforcing our commitment to sustainable green manufacturing.
Established in 2014 with a registered capital of 120 million yuan, Shandong Kawah Oils Co., Ltd. is a provincial leading agricultural industrialization enterprise. Processing 180,000 tons of NON-GMO domestic soybeans annually, we extract non-GMO soybean oil, low-temperature food-grade soybean meal, isolated soy protein, and soluble dietary fiber with clinical-grade precision. Our core technological advantage lies in our industry-leading spray drying tower supplied by DACHUANYUAN, featuring a single-line capacity that ranks as the largest in China, guaranteeing unmatched batch uniformity and structural stability.
Founded in 2011 with 6 million yuan of registered capital, Guanxian Ruichang Trading Co., Ltd. acts as the direct international bridge connecting our manufacturing plants with worldwide clientele. Exporting isolate soy protein, wheat gluten, soluble dietary fiber, vermicelli, and ethanol directly from factory floors, over 70% of our group's total production capacity is channeled to international markets across North America, Europe, Southeast Asia, and the Middle East.
The global transition toward sustainable, plant-based nutrition has accelerated exponentially. As consumers increasingly prioritize clean-label foods, functional beverages, and sports nutrition, food manufacturers face unprecedented demands for high-purity protein ingredients. Market intelligence indicates a compound annual growth rate (CAGR) exceeding 8% for isolated soy protein and vital wheat gluten sectors through 2030.
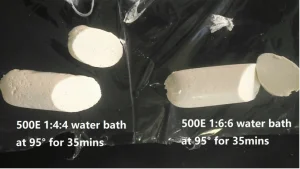
To address complex industrial formulation challenges—such as emulsion stability in meat analogs, heat resistance in bakery items, and smooth mouthfeel in RTD (Ready-to-Drink) beverages—Xinrui Group delivers highly tailored macro-solutions. Our specialized grades (such as the 9007B series for meat emulsification, 9030 series for beverage dispersion, and VWG-PS pellets for bakery texture enhancement) are engineered to meet exacting rheological and nutritional parameters.
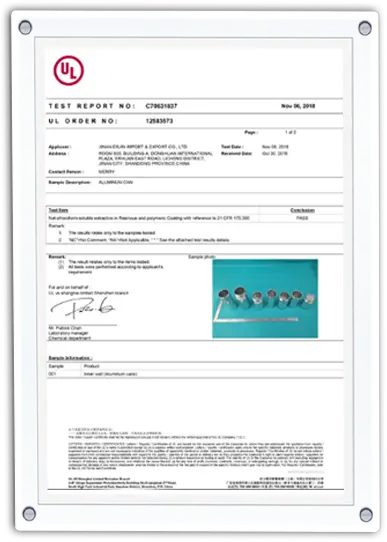
Navigating international regulatory frameworks requires rigorous compliance protocols. Our manufacturing facilities maintain world-class quality management certifications, ensuring seamless customs clearance and regulatory approval in destination markets worldwide.
Looking ahead, Xinrui Group is heavily investing in enzymatic protein modification, nano-filtration purification, and carbon-neutral processing technologies. Our R&D pipeline focuses on allergen-reduced plant proteins, enhanced solubility profiles, and synergistic hydrocolloid blends designed to empower next-generation functional foods and nutritional supplements.
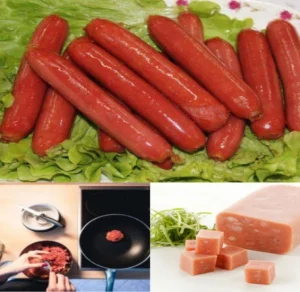
We are a fully integrated group company named Xinrui Group that combines large-scale manufacturing and direct global exporting. Specifically:
• Soy Protein Isolate Manufacturer: Shandong Kawah Oils Co., Ltd., producing 50,000 tons of isolated soy protein annually.
• Wheat Gluten Manufacturer: Guanxian Xinrui Industrial Co., Ltd. (formerly Guanxian Ruixiang Biotechnology Development Co., Ltd.), producing 30,000 tons of vital wheat gluten annually.
• Global Exporter: Guanxian Ruichang Trading Co., Ltd.
We maintain rigorous international quality standards and hold HACCP, ISO9001, ISO22000, BRC, HALAL, KOSHER, IP-NON GMO, and SGS certifications. Additional specific regulatory or custom documentation can be provided upon request.
MOQ typically aligns with standard container loads (20ft FCL) to optimize freight efficiency for our global wholesale clients. Lead times vary from 14 to 25 days depending on destination port and specific product formulation requirements. Contact our export sales team for customized logistical solutions.
 Xinrui Group